Battery Cell Sealing Explained: How Lithium-Ion Cells Are Closed and Protected
Understanding Cell Sealing, Leak Prevention, Moisture Protection, Packaging Integrity, and Quality Control in Lithium-ion Battery Manufacturing
Category: Battery Technology
Content Type: Manufacturing
Learning Path: Battery Manufacturing
Related Industries: Electric Vehicles · Energy Storage Systems · Consumer Electronics
Last Updated: September 2026
Industry Snapshot
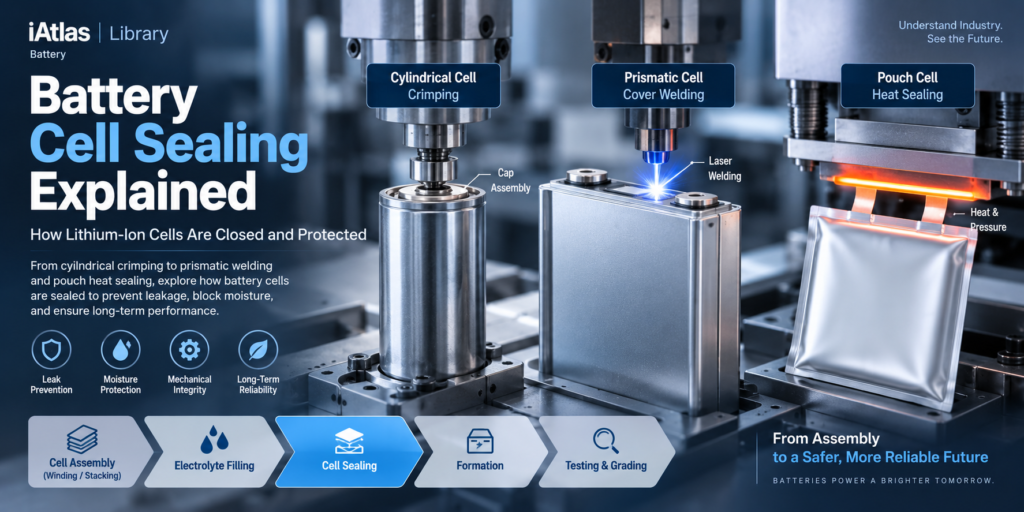
Battery cell sealing is the manufacturing process that closes a lithium-ion battery cell after its internal electrode assembly and electrolyte have been installed.
The purpose of sealing is not simply to close the battery.
The finished cell must maintain a controlled internal environment throughout manufacturing and operation while limiting:
- Electrolyte leakage
- Moisture ingress
- External contamination
- Uncontrolled gas escape
- Mechanical damage
The exact sealing process depends strongly on cell format.
Cylindrical Cell
→ Metal can + cap assembly
Prismatic Cell
→ Rigid housing + cover plate
Pouch Cell
→ Multilayer flexible pouch + heat-sealed edges
This makes sealing one of the points where cell design and manufacturing process become closely interconnected.
At a Glance
| Category | Description |
|---|---|
| Process | Battery Cell Sealing |
| Stage | Cell Assembly |
| Input | Electrode Assembly + Electrolyte + Cell Housing |
| Main Function | Close and protect the internal cell environment |
| Key Requirements | Leak Tightness · Moisture Protection · Mechanical Integrity |
| Typical Methods | Welding · Crimping · Heat Sealing |
| Major Risks | Leakage · Weak Seal · Contamination · Misalignment |
| Previous Process | Electrolyte Filling |
| Next Major Stage | Formation |
What Is Battery Cell Sealing?
Battery cell sealing creates the physical barrier between the internal electrochemical system and the external environment.
Inside the cell are:
Cathode
Separator
Anode
Electrolyte
These components must operate within a carefully controlled environment.
The enclosure provides:
Mechanical Protection
Environmental Isolation
Electrolyte Containment
Electrical Interface
Sealing completes this enclosure.
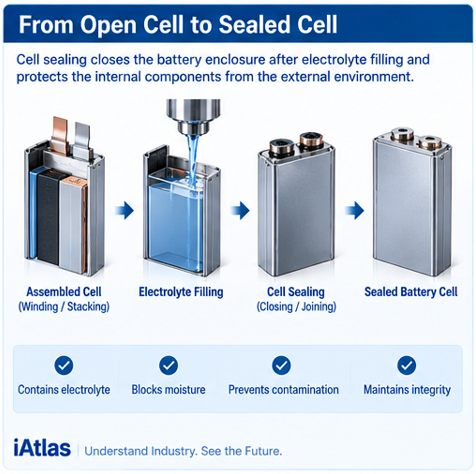
A simplified process is:
Assembled Cell
↓
Electrolyte Filling
↓
Seal Interface Preparation
↓
Closing / Joining
↓
Seal Inspection
↓
Closed Battery Cell
Why Battery Cells Must Be Sealed
Lithium-ion batteries contain materials that should remain isolated from the uncontrolled external environment.
An effective seal serves several purposes.
Electrolyte Containment
Liquid electrolyte must remain inside the cell.
Moisture Protection
External humidity should not freely enter the cell.
Contamination Control
Particles and external contaminants must be prevented from entering after assembly.
Mechanical Integrity
The housing must remain structurally stable during handling and operation.
Controlled Internal Environment
The cell’s internal chemical environment must remain within the intended design conditions.
Therefore:
Cell sealing is both a packaging process and a battery-quality process.
Where Cell Sealing Fits in Battery Manufacturing
Using our iAtlas Manufacturing Learning Path:
Electrode Manufacturing
Material Mixing
→ Battery Slurry
→ Electrode Coating
→ Electrode Drying
→ Calendering
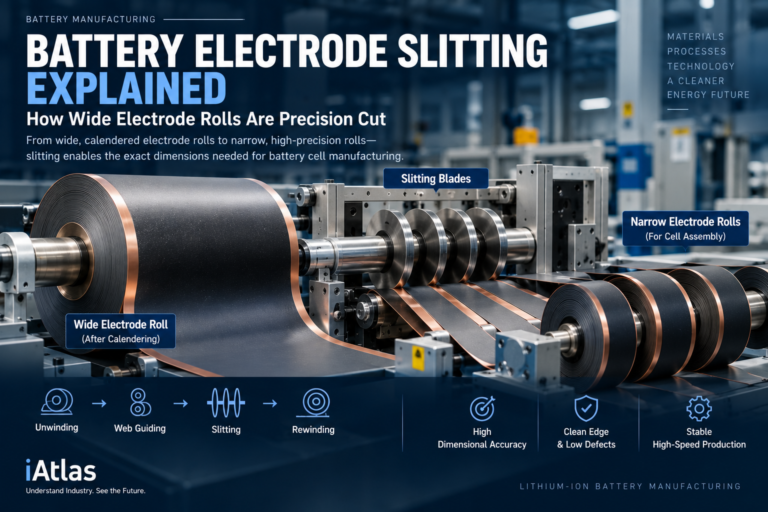
→ Slitting
Cell Assembly
Battery Cell Assembly
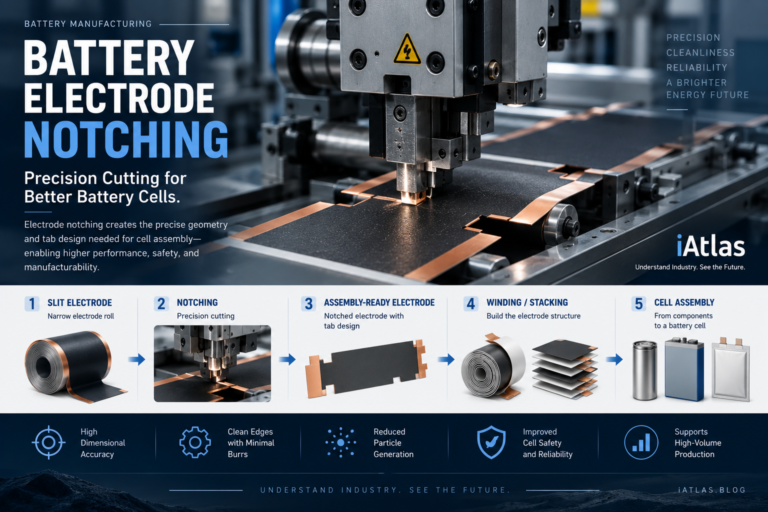
→ Notching
→ Winding / Stacking
→ Electrolyte Filling
→ Cell Sealing
Cell Finishing
Formation
→ Aging
→ Degassing
→ Testing & Grading
However, the exact sequence is cell-format dependent.
For example, pouch cells can undergo an initial sealing operation before formation and later require degassing and final sealing.
So Cell Sealing should be understood as a manufacturing function rather than one universally identical step across all battery formats.
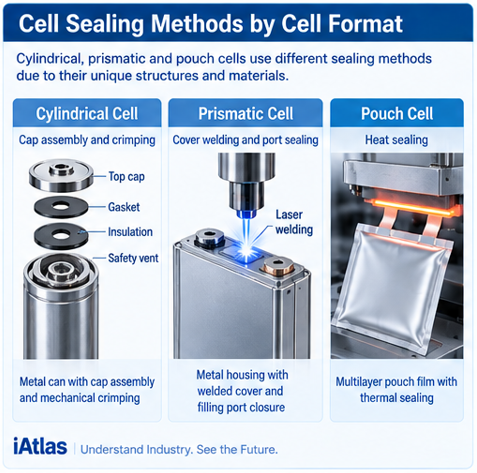
Cell Sealing Depends on Cell Format
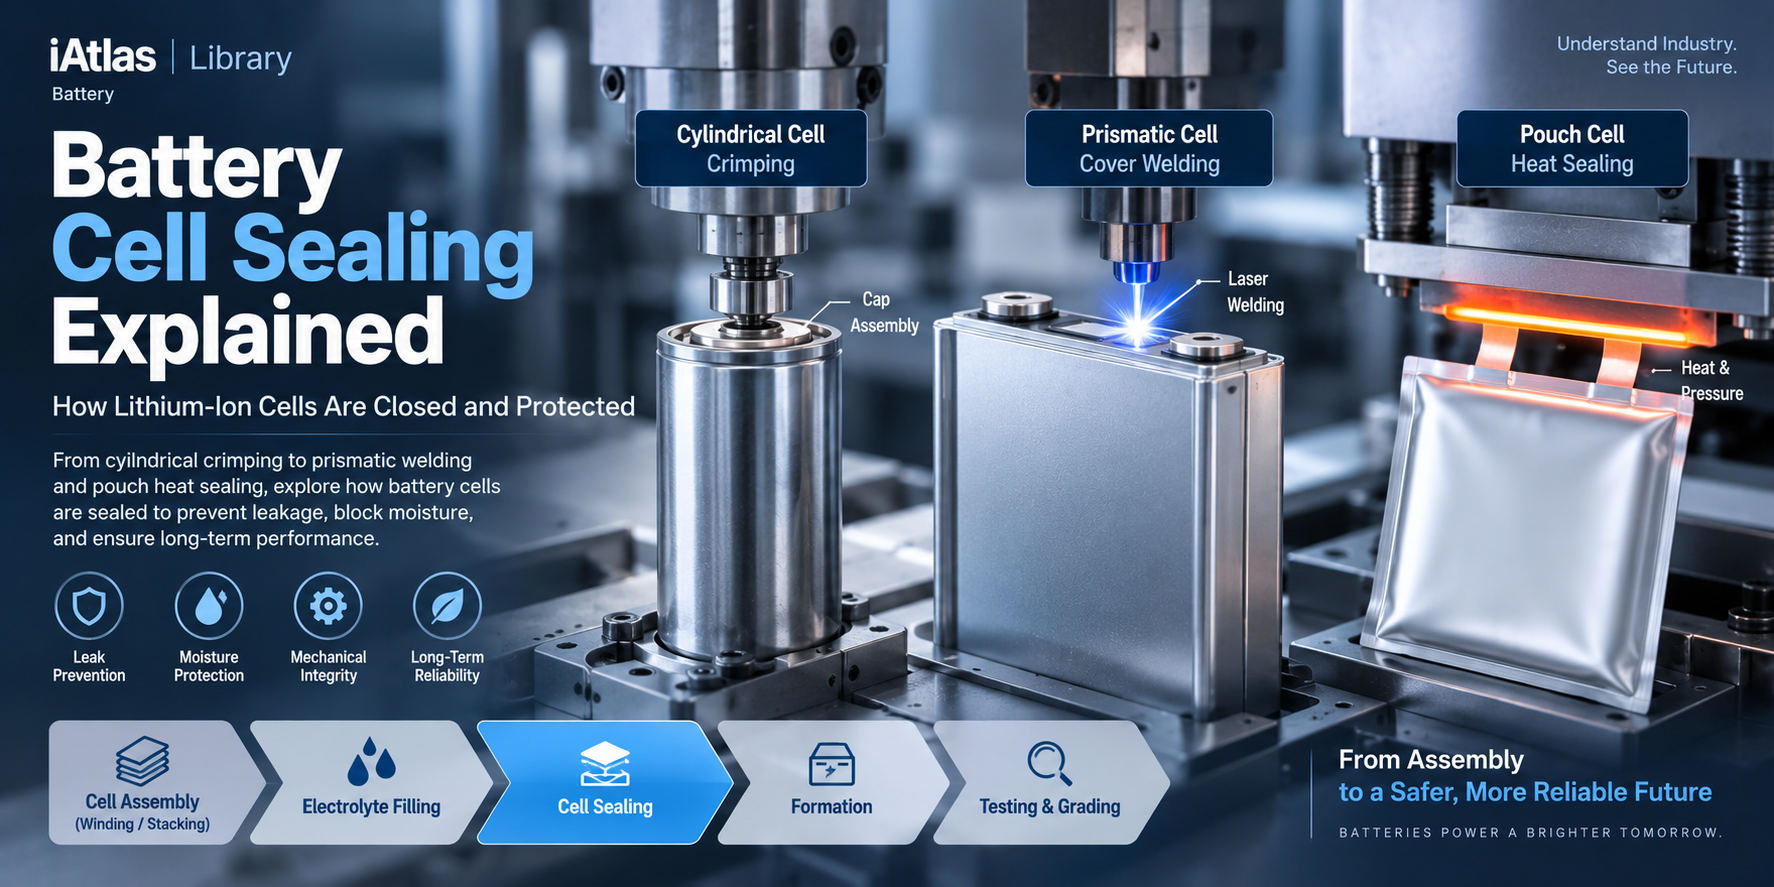
The three major lithium-ion cell formats require different sealing strategies.
| Cell Format | Housing | Typical Sealing Concept |
|---|---|---|
| Cylindrical | Metal can | Cap assembly / crimping / joining |
| Prismatic | Rigid metal housing | Cover plate joining / welding |
| Pouch | Multilayer laminate film | Thermal sealing |
The sealing method must match:
- Housing material
- Cell geometry
- Terminal structure
- Electrolyte filling architecture
- Gas-management strategy
- Production process
Cylindrical Cell Sealing
Cylindrical cells use a rigid metal can.
After the jelly roll has been inserted and the required internal assembly operations have been completed, the cell must be closed with a cap assembly.
Conceptually:
Jelly Roll
↓
Metal Can
↓
Electrolyte Filling
↓
Cap Assembly
↓
Closing / Crimping
↓
Sealed Cylindrical Cell
The cap region may integrate several functions beyond simple closure, depending on cell design.
These can include:
- Electrical terminal
- Insulation components
- Gasket
- Safety vent
- Current-interruption features
This makes the top closure of a cylindrical cell a highly engineered assembly.
The Role of the Gasket
A gasket can help electrically and physically isolate components around the cylindrical cell closure.
Its functions can include:
Electrical Insulation
Seal Support
Mechanical Interface
The gasket must withstand the mechanical conditions created during cell closing while maintaining the intended isolation and sealing characteristics.
Incorrect positioning or damage can compromise cell quality.
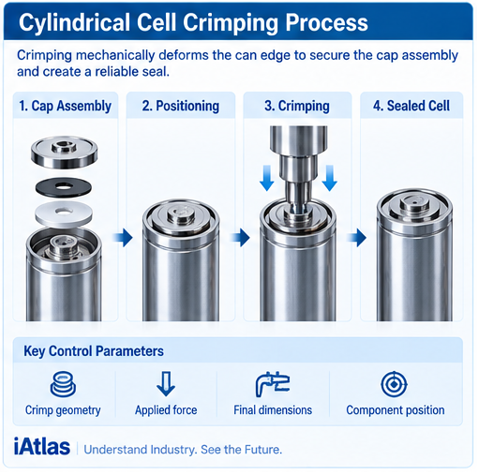
Cylindrical Cell Crimping
Crimping mechanically deforms the upper portion of the cell can around the cap assembly.
Conceptually:
Can + Cap + Gasket
↓
Controlled Mechanical Force
↓
Can Edge Deformation
↓
Compressed Closure
The process must control parameters such as:
- Crimp geometry
- Applied force
- Final dimensions
- Component position
Too little deformation may create inadequate closure.
Excessive deformation can damage components or alter the intended geometry.
Prismatic Cell Sealing
Prismatic cells generally use a rigid rectangular housing.
The electrode stack or wound assembly is installed inside the housing and connected to the terminal structure.
A simplified sequence is:
Electrode Assembly
↓
Prismatic Housing
↓
Cover Plate
↓
Joining / Welding
↓
Electrolyte Filling
↓
Fill-Port Closure
The exact order varies with cell design.
One important distinction is that the main cover may already be joined before electrolyte filling.
Electrolyte can then be introduced through a dedicated filling port.
After filling, that opening must also be closed.
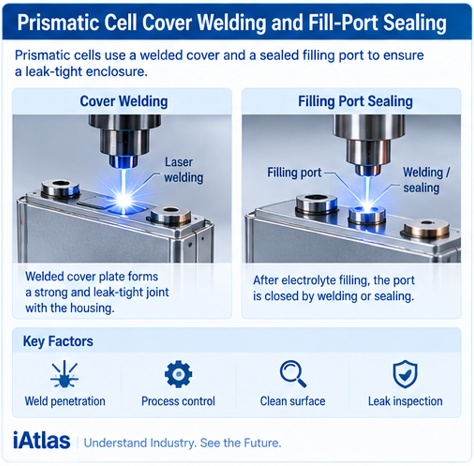
Prismatic Cover Welding
The cover plate must form a strong and sufficiently leak-tight joint with the cell housing.
Laser welding is one technology used in battery manufacturing for this type of precision joining.
A simplified concept is:
Cover Plate
↓
Precisely Positioned on Housing
↓
Laser Welding
↓
Continuous Weld Seam
↓
Inspection
Important factors include:
- Weld penetration
- Seam continuity
- Heat input
- Surface cleanliness
- Component fit
- Welding speed
The objective is a consistent joint without creating unacceptable thermal or structural damage.
Electrolyte Filling Port Sealing
Rigid battery cells may use a small opening for electrolyte filling.
After the required electrolyte has been introduced:
Filling Port
↓
Closure Component
↓
Welding / Sealing
↓
Leak Inspection
This small region can be critical because the cell is otherwise largely closed.
A defect around the fill port can compromise the integrity of the entire cell.
Pouch Cell Sealing
Pouch cells use a flexible multilayer laminate rather than a rigid metal can.
The electrode stack is placed inside the pouch material.
Conceptually:
Electrode Stack
↓
Pouch Film
↓
Electrolyte Filling
↓
Heat Sealing
↓
Formation
↓
Degassing
↓
Final Sealing
This architecture makes the pouch sealing process fundamentally different from rigid-cell closure.
How Pouch Heat Sealing Works
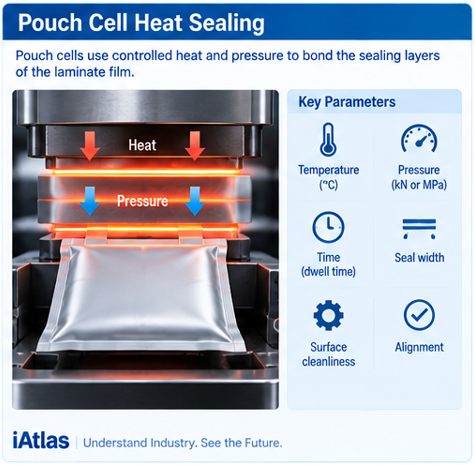
Pouch sealing typically uses controlled heat and pressure to bond compatible sealing layers of the laminate.
A simplified process is:
Pouch Layers
↓
Heat
Pressure
Time
↓
Bonded Seal
The key manufacturing variables therefore include:
- Temperature
- Pressure
- Dwell time
- Seal width
- Surface condition
- Alignment
These variables must remain within the intended process window.
Why Seal Temperature Matters
If the sealing temperature is too low:
Insufficient Melting / Bonding
↓
Weak Seal
If temperature is too high:
Excessive Thermal Exposure
↓
Film Damage / Seal Deformation Risk
The objective is therefore not maximum heat.
It is:
A controlled thermal window that creates a consistent bond without damaging the pouch structure.
Why Seal Pressure Matters
Heat alone is not sufficient.
The pouch layers must be pressed together while the sealing surfaces form their bond.
Insufficient pressure can result in incomplete contact.
Excessive pressure can deform the sealing region or affect the laminate structure.
Therefore:
Temperature + Pressure + Time
must be controlled together.
Seal Surface Cleanliness
The sealing surfaces must be sufficiently clean before joining.
Potential contaminants include:
- Electrolyte
- Electrode particles
- Dust
- Foreign material
For example:
Contaminant at Seal Interface
↓
Incomplete Contact
↓
Local Weak Region
↓
Potential Leakage Path
This is particularly important during electrolyte filling because liquid electrolyte is being handled near the eventual sealing region.
Electrolyte Contamination of the Seal Area
A key challenge in pouch-cell manufacturing is preventing electrolyte from contaminating the sealing interface.
If electrolyte reaches the heat-seal region before closure, it can interfere with consistent bonding.
Manufacturing equipment therefore needs to coordinate:
Electrolyte Dosing
Cell Position
Seal-Area Cleanliness
Sealing
This illustrates why filling and sealing cannot be optimized completely independently.
Tab Sealing in Pouch Cells
Pouch cells have electrical tabs extending through the pouch boundary.
This creates a challenging sealing region.
The seal must transition around the tab while maintaining the required barrier.
Conceptually:
Pouch Film
→ Tab Interface → Pouch Film
The tab region may require dedicated sealing materials or structures to maintain compatibility between the metal tab and pouch laminate.
This region is therefore an important quality-control point.
Common Battery Cell Sealing Defects
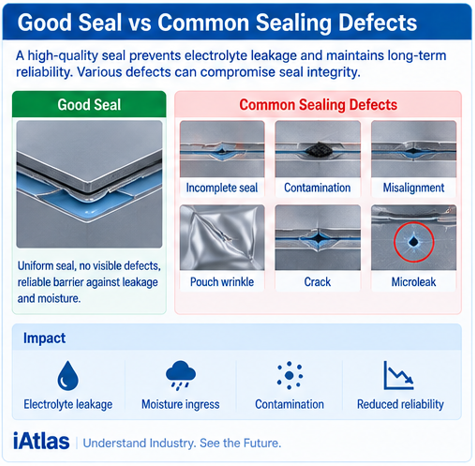
Several defects can compromise cell sealing.
Incomplete Seal
Part of the sealing interface does not fully join.
Seal Misalignment
Components are not positioned correctly.
Contamination
Foreign material or electrolyte remains within the sealing interface.
Weak Weld
The joining process does not produce sufficient mechanical integrity.
Excessive Heat Input
Thermal damage occurs around the joining region.
Pouch Wrinkle
The laminate folds or wrinkles during sealing.
Tab-Seal Defect
The interface around the electrical tab is incomplete.
Microleak
A very small leakage pathway exists even though the cell appears externally closed.
What Is a Microleak?
Not every sealing defect produces obvious visible leakage.
A microscopic pathway can allow very small quantities of material to move through the enclosure over time.
This is a microleak.
Conceptually:
Apparently Closed Seal
↓
Microscopic Defect
↓
Slow Gas / Vapor / Electrolyte Transport
↓
Long-Term Reliability Risk
This is why visual inspection alone cannot guarantee seal integrity.
Leak Testing
Battery manufacturers can use leak testing to verify enclosure integrity.
Depending on the cell and process, methods can involve:
- Pressure-decay testing
- Vacuum-based testing
- Tracer-gas methods
- Helium leak detection
- Other gas-based detection methods
The required sensitivity depends on the cell design and quality specification.
Leak testing converts sealing quality from a purely visual judgment into a measurable production parameter.
Helium Leak Testing
Helium is useful as a tracer gas because very small leak paths can potentially be detected with sensitive instrumentation.
Conceptually:
Cell / Test Chamber
↓
Helium Exposure or Internal Tracer
↓
Leak Detector
↓
Measured Leak Rate
This can help identify defects that would be difficult to detect visually.
However, the exact test architecture depends on the production process and cell design.
Vision Inspection
Machine vision can inspect external sealing characteristics.
Possible inspection targets include:
- Weld position
- Seal width
- Surface defects
- Pouch wrinkles
- Component alignment
- Fill-port closure
- Tab position
A typical automated system is:
Sealed Cell
↓
Camera / Sensor
↓
Image Analysis
↓
Defect Classification
↓
Accept / Reject
Vision inspection complements rather than necessarily replaces leak testing.
Weld Inspection
For welded metal housings, manufacturers may evaluate:
- Weld geometry
- Surface appearance
- Seam continuity
- Penetration characteristics
- Porosity
- Cracks
Some measurements can be performed inline, while others may require sampling or destructive analysis.
Increasingly, welding equipment also records process data such as laser power, speed, and other signals for traceability.
Moisture Protection
One of the main purposes of cell sealing is preventing uncontrolled exposure to external humidity.
Moisture can interact with electrolyte components and negatively affect battery chemistry.
Therefore:
Dry Manufacturing Environment
↓
Electrolyte Filling
↓
Cell Sealing
↓
Controlled Internal Environment
The sealing process effectively preserves the carefully controlled conditions created during earlier dry-room manufacturing.
Mechanical Integrity
The cell enclosure also has a structural role.
During later stages, the battery may experience:
- Handling
- Formation
- Internal gas generation
- Thermal cycling
- Vehicle vibration
- Mechanical loads
The seal must remain compatible with these conditions.
This means sealing quality is not only about initial leak tightness.
It also relates to long-term mechanical reliability.
Why Gas Management Complicates Sealing
Battery cells can generate gas during formation and operation.
Therefore, sealing strategy must consider not only keeping external materials out but also managing internal pressure.
Different cell formats approach this differently.
Cylindrical / Prismatic
May integrate engineered safety venting features.
Pouch
Can undergo formation with a temporary gas pocket followed by degassing and final sealing.
This is why pouch-cell manufacturing includes the later Degassing step in our Learning Path.
Initial Sealing vs Final Sealing in Pouch Cells
Pouch cells illustrate why “cell sealing” is not always one single event.
A simplified sequence is:
Electrolyte Filling
↓
Initial Sealing
↓
Formation
↓
Gas Generation
↓
Degassing
↓
Final Sealing
The temporary gas space allows gases produced during initial electrochemical reactions to be collected and later removed.
After degassing, the pouch can be permanently resealed and trimmed according to the cell design.
Quality Control During Cell Sealing
Modern sealing processes can monitor multiple variables.
Position
Are components correctly aligned?
Temperature
Is the heat-sealing temperature within the process window?
Pressure
Is appropriate force applied?
Time
Is the dwell time consistent?
Welding Parameters
Are laser power, speed, and focal conditions controlled?
Seal Geometry
Is the seal width and shape correct?
Leak Rate
Does the cell meet the required leak specification?
Visual Condition
Are wrinkles, cracks, contamination, or other defects present?
Process Traceability
Modern battery production increasingly records process parameters for individual cells or production lots.
For sealing, these data may include:
Cell ID
Welding / Sealing Parameters
Inspection Result
Leak Test
Timestamp / Equipment Data
This enables manufacturers to connect downstream failures with upstream process history.
From Cell Sealing to Formation
Once the cell has been appropriately closed for its manufacturing architecture, it proceeds toward one of the most important finishing processes:
Formation
Formation is the first controlled electrochemical charging process used to establish important interfaces inside the battery.
The sequence now becomes:
Electrode Manufacturing
↓
Cell Assembly
↓
Electrolyte Filling
↓
Cell Sealing
↓
Formation
This represents a major transition.
Until this point, battery manufacturing has been dominated primarily by:
Materials + Mechanical Processing + Assembly
Formation introduces:
Electrochemical Processing
The next iAtlas Library article will examine this transition in detail.
Emerging Battery Cell Sealing Technologies
Battery sealing continues to evolve alongside cell design.
Advanced Laser Welding
Higher-precision laser systems can improve control of metal housing joints.
Inline Weld Monitoring
Optical and process signals can be analyzed during welding.
Automated Leak Detection
High-throughput leak-testing systems can integrate directly into production lines.
Machine Vision
AI-assisted image analysis can improve defect classification.
Digital Traceability
Seal parameters can be linked to each cell’s manufacturing history.
Larger Cell Formats
Larger cylindrical and prismatic cells create new requirements for welding geometry, dimensional control, and thermal management during joining.
The overall trend is:
Joining
Inspection
Process Data
becoming increasingly integrated.
iAtlas Insight
Cell sealing is easy to underestimate because it occurs near the end of mechanical cell assembly.
But its function is unusually important.
Before sealing, manufacturers invest heavily in controlling:
Electrode Quality
→ Particle Contamination
→ Alignment
→ Electrolyte Quantity
→ Moisture
All of those carefully controlled conditions eventually depend on the enclosure maintaining its integrity.
This creates a simple manufacturing relationship:
High-Quality Internal Cell
Poor Seal
=
Poor Battery
As battery manufacturers move toward larger cells, higher energy densities, and faster production, sealing becomes increasingly connected with precision joining, inline inspection, leak detection, and manufacturing data.
The seal is therefore not merely the last step that closes a container.
It is the boundary that preserves everything created by the upstream battery manufacturing process.
Did You Know?
- Cylindrical, prismatic, and pouch cells use fundamentally different sealing architectures.
- Pouch cells can undergo both initial and final sealing.
- Prismatic cells can be filled through a dedicated electrolyte filling port after the main cover has been joined.
- A cell can have a sealing defect even when no visible electrolyte leakage is present.
- Leak testing and visual inspection measure different aspects of sealing quality.
- Pouch-cell tab regions are particularly important sealing interfaces.
- Cell sealing preserves the low-moisture internal environment established during manufacturing.
- After cell assembly and sealing, manufacturing transitions toward electrochemical processing during formation.
FAQ
What is battery cell sealing?
Battery cell sealing is the manufacturing process used to close the cell enclosure and protect the internal electrodes and electrolyte from the external environment.
Why must lithium-ion battery cells be sealed?
The seal helps contain electrolyte, prevent unwanted moisture and contamination ingress, and maintain the intended internal environment.
How are cylindrical battery cells sealed?
Cylindrical cells typically use a metal can and cap assembly with mechanical closing or crimping and associated sealing components.
How are prismatic battery cells sealed?
Prismatic cells generally use a rigid metal housing with a welded cover. A separate electrolyte filling port may subsequently be sealed.
How are pouch cells sealed?
Pouch cells use thermal sealing of multilayer laminate packaging.
Why are pouch cells degassed after formation?
Initial electrochemical reactions can generate gases. Pouch manufacturing can provide a temporary gas space that is opened during degassing before final sealing.
What is a battery microleak?
A microleak is a very small leakage pathway through the cell enclosure or seal that may not be visible externally.
How is battery sealing quality tested?
Methods can include visual inspection, machine vision, dimensional inspection, weld analysis, pressure or vacuum testing, and tracer-gas leak detection.
What comes after cell sealing?
In the iAtlas Battery Manufacturing Learning Path, the next major process is Battery Formation.
Battery Manufacturing Learning Path
Overview
Electrode Manufacturing
Cell Assembly
- Battery Cell Assembly
- Battery Electrode Notching
- Battery Electrode Winding
- Battery Electrode Stacking
- Battery Electrolyte Filling
- Battery Cell Sealing (Current)
Cell Finishing
- Formation
- Aging
- Degassing
- Battery Cell Testing & Grading
System Assembly
- Battery Module Assembly
- Battery Pack Assembly
Explore More
Cell Assembly
- Battery Cell Assembly
- Battery Electrode Notching
- Battery Electrode Winding
- Battery Electrode Stacking
- Battery Electrolyte Filling
- Battery Cell Sealing (Current)
Electrode Manufacturing
Battery Components
- Cathode
- Anode
- Separator
- Electrolyte
- Battery Cell
References
VDMA / PEM RWTH Aachen — Production Process of a Lithium-Ion Battery Cell
VDMA — Production Process of a Lithium-Ion Battery Cell
PEM RWTH Aachen University — Battery Production Research
PEM RWTH Aachen — Battery Production
Fraunhofer ILT — Laser Processing in Battery Production
Fraunhofer ILT — Battery Production Technology
TWI — Battery Joining Technologies
TWI — Battery Joining and Welding Technology
About iAtlas
iAtlas is an independent publication covering batteries, semiconductors, OLED, advanced materials, AI, and global industrial trends.
We transform complex industrial developments into clear, reliable, and easy-to-understand insights.
Whether you’re following today’s industry news or building long-term expertise, iAtlas helps you understand not only what happened, but why it matters.
Technology creates change.
Insight creates opportunity.
— iAtlas